Titanium Welding Wire for Heat Exchanger and Chemical Equipment Fabrication
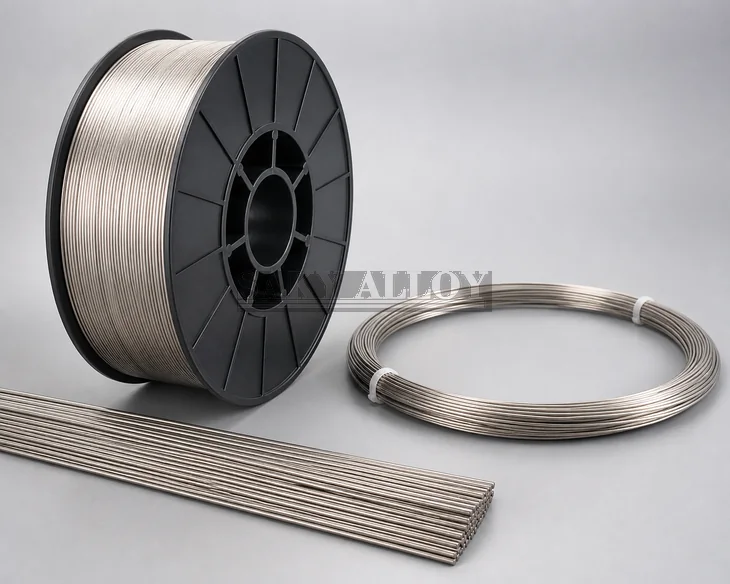
Titanium welding wire must be selected with the base metal, joint design, qualified welding procedure, service environment and construction code. Define ERTi classification, diameter, delivery form, cleanliness, lot traceability and certificate before production welding.
Application and Filler Matrix
| Joint context | Initial filler review | Required confirmation |
|---|---|---|
| Grade 2 equipment | ERTi-2 commonly evaluated | Base specification, service, WPS/PQR and code |
| Grade 7 corrosion service | ERTi-7 may support compatible palladium-alloyed fabrication | Corrosion design and qualified procedure |
| Ti-6Al-4V components | ERTi-5 belongs to the compatible alloy family | Strength, heat input, joint properties and procedure |
| Dissimilar titanium grades | Engineering-selected filler | Both base metals, service, code and qualification tests |
Heat Exchanger and Process Equipment Data
Identify tube-to-tube-sheet, pipe, plate or fitting joint; base-metal grades and standards; medium and temperature; pressure code; joint design; welding process; and required corrosion behavior. Matching a trade name alone does not establish an acceptable filler.
Cleanliness, Shielding and Storage
Titanium is sensitive to oxygen, nitrogen, hydrogen, grease and dirt at elevated temperature. Control wire storage, joint cleaning, gas purity, primary/trailing/root shielding, interpass condition and feeding. Define discoloration acceptance and repair rules in the fabrication procedure.
Form, Package and Documentation
State straight rod, spool or coil, diameter and tolerance, rod length or spool dimensions, unit weight and quantity. Packaging should prevent moisture, dirt, damage and mixed-lot use. Require classification certificate and heat/lot traceability.
Match Filler to the Qualified Procedure
Compare ERTi-2, ERTi-5 and ERTi-7 Welding Wire.
RFQ Checklist
- Base metal, joint, process and governing code
- ERTi classification and invoked specification
- Diameter, form, package weight and quantity
- WPS/PQR and service requirements
- Certificate, lot traceability and packaging
FAQ
Can filler be selected only from base grade?
No. Joint, service, code and qualified procedure also control selection.
Can ASTM B863 wire replace AWS-classified filler?
Not by assumption. The order and procedure must require the correct filler classification.
Why protect opened packages?
Cleanliness and lot control help prevent weld contamination and material mix-up.
Related Reading
ERTi-2 vs ERTi-5 vs ERTi-7 · ASTM B338 Tube RFQ · Titanium Welding Basics
Match the Filler Classification Before Requesting a Quote
Do not select welding consumable from the base-metal grade name alone. Confirm the governing filler-metal classification, base metals to be joined, wire diameter, process, spool or straight-length form, package weight, quantity and required lot documentation.
- ERTi-1 / Grade 1 titanium welding wire for applicable commercially pure titanium welding procedures.
- ERTi-2 titanium welding wire for procedures that expressly require the ERTi-2 filler classification.
- ERTi-5 Ti-6Al-4V welding wire where the qualified procedure requires ERTi-5.
For pricing, send the complete welding-wire RFQ through Contact SAKY ALLOY. Any filler substitution requires approval of the applicable welding procedure and engineering requirements.